
Every manufacturer knows the cost of a defect that escapes the factory. Returns, rework, warranty claims and damaged customer trust all add up far faster than the price of catching the problem early. Artificial intelligence is changing how that early catch happens. Instead of relying on tired eyes at the end of a shift, modern vision systems examine every single item on the line, in real time, and flag anything that looks wrong. For plants considering the jump, the hardest question is usually not whether the technology works, but where to begin.
What AI Adds to Traditional Machine Vision
Conventional machine vision relies on fixed rules: measure this edge, check this colour, confirm this barcode. It works well when products are identical and conditions never change, but it struggles with natural variation such as textured surfaces, reflective finishes or subtle cosmetic flaws. AI-based inspection learns from labelled example images instead. Show it enough good and bad parts and it begins to recognise the difference on its own, including defects nobody wrote a rule for. That makes it particularly valuable for products where “acceptable” has a wide range and “faulty” is hard to define in numbers.
Pick One High-Value Problem First
The most successful projects start small. Rather than trying to automate every inspection point at once, choose a single stage where defects are costly, frequent or hard for people to spot consistently. Good candidates include surface finish checks, assembly verification (is every component present and correctly seated?), label and print quality, and seal or weld integrity. A narrow, well-defined target makes it easier to collect training images, measure results and prove the return on investment before expanding.
Lighting and Hardware Matter as Much as the Software
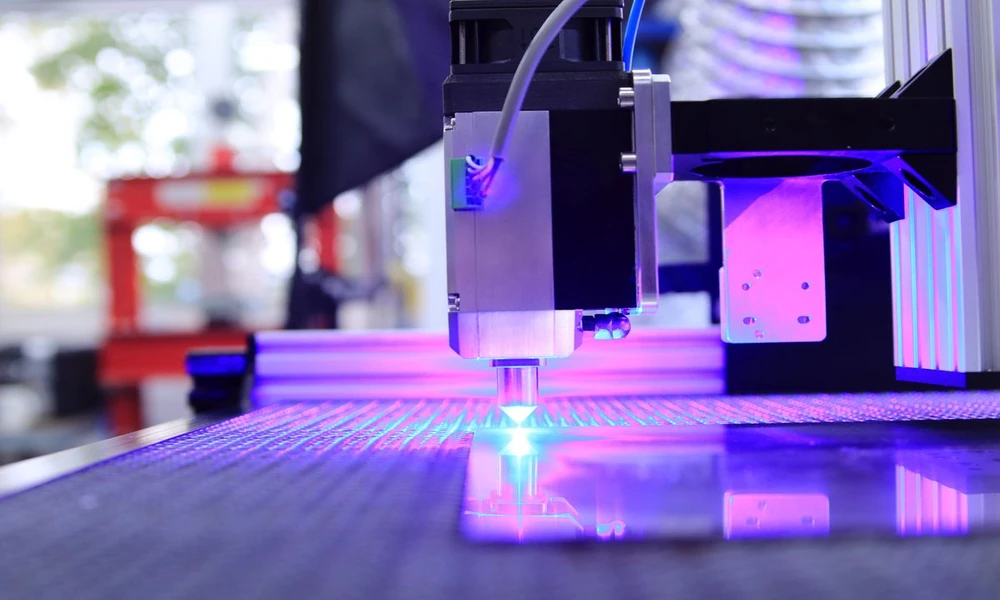
A common mistake is assuming the AI model will compensate for poor imaging. In reality, consistent lighting, the right camera resolution and stable mounting often decide whether a system succeeds. Experienced integrators such as Industrial Vision Systems spend as much time on optics, illumination and line integration as on the software itself, because a clean, repeatable image is what lets an AI model perform reliably day after day.
Connect Inspection to the Wider Production Picture
A vision system that only rejects bad parts leaves value on the table. When inspection results feed back into production data, patterns start to appear: a particular machine drifting out of tolerance, a batch of raw material causing more flaws, or a shift change that coincides with more defects. Fixing the cause is far cheaper than endlessly sorting the symptoms.
That joined-up thinking applies across the plant floor. Our recent look at the benefits of pallet filling systems for bulk production shows how tightly linked filling, handling and quality steps can become when equipment shares data rather than operating in isolation.
Plan for People, Not Just Machines
Introducing AI inspection changes roles rather than simply removing them. Operators become the people who review flagged exceptions, confirm borderline cases and help retrain the model as products evolve. Involving them early, explaining what the system does and asking for their knowledge of typical defects makes the rollout smoother and the model more accurate.
It also helps to look at what peers are doing. Industry body Make UK publishes research and guidance on manufacturing technology adoption, which can help smaller firms benchmark their plans and avoid common pitfalls.
A Practical Checklist Before You Start
- Define the defect. Agree what counts as acceptable and unacceptable, with example images.
- Gather representative data. Capture good and faulty parts across shifts, batches and lighting conditions.
- Set measurable goals. Track detection rate, false rejects and the cost of escapes.
- Pilot before scaling. Run the system alongside manual inspection to build confidence.
The Bottom Line
AI-powered vision inspection is no longer reserved for the largest factories. Falling hardware costs and more flexible software mean mid-sized manufacturers can now justify the investment, provided they start with a clear problem, invest in good imaging and bring their people along. Get those foundations right, and the payoff is fewer defects, less waste and far greater confidence in every product that leaves the line.